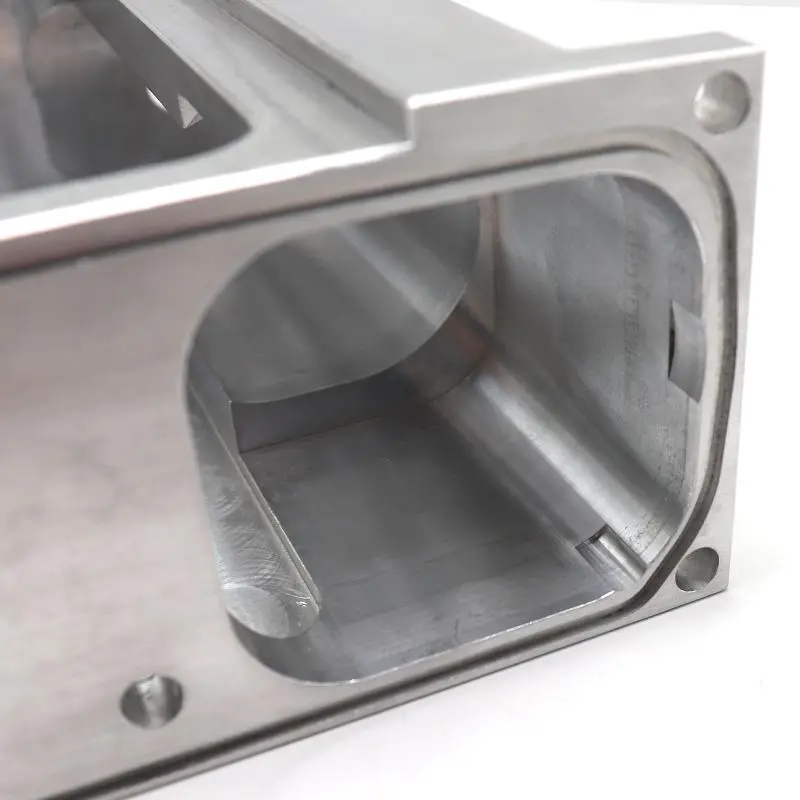
Deep Pockets
Deep cavities, stepped pockets, recessed surfaces, and internal profiles with defined wall thicknesses and corner radii.
We provide custom CNC milling services for prototypes, small batches, and ongoing production. From initial samples to repeat orders, we manufacture parts to your drawings and specifications.
MS Machining provides CNC milling for custom parts requiring machining on multiple faces, angled surfaces, and features with specific positional relationships. Machining setups are selected according to part geometry, tool access, and drawing requirements.
| Milling Processes | 3-Axis, 4-Axis & 5-Axis CNC Milling |
|---|---|
| 3-Axis Maximum Part Size | 800 × 400 × 400 mm |
| 4-Axis Maximum Part Size | 700 × 400 × 350 mm |
| 5-Axis Maximum Part Size | Ø500 × H300 mm |
| Multi-Side Machining | Multi-face machining, rotary-axis positioning and simultaneous 5-axis machining |
| Production Scope | Custom Prototypes, Small Batches & Repeat Production |
Maximum part size depends on geometry, material, workholding and tool access. Final machining feasibility is confirmed after drawing review.
MS Machining provides CNC milling for custom parts with deep cavities, thin walls, narrow slots, and complex surface geometries. We also support multi-sided features, precision holes, and machined interfaces for assembly applications.
Deep cavities, stepped pockets, recessed surfaces, and internal profiles with defined wall thicknesses and corner radii.
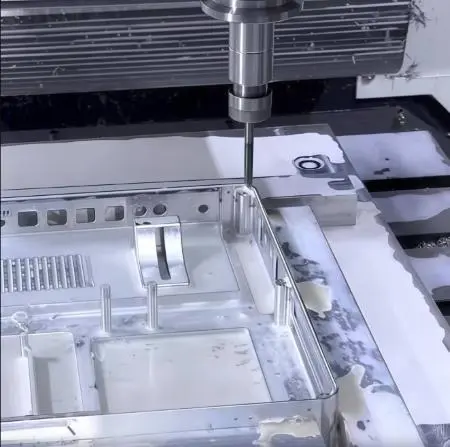
Thin-wall housings, ribs, and structural features with wall thicknesses down to 0.5 mm, depending on part geometry and material.
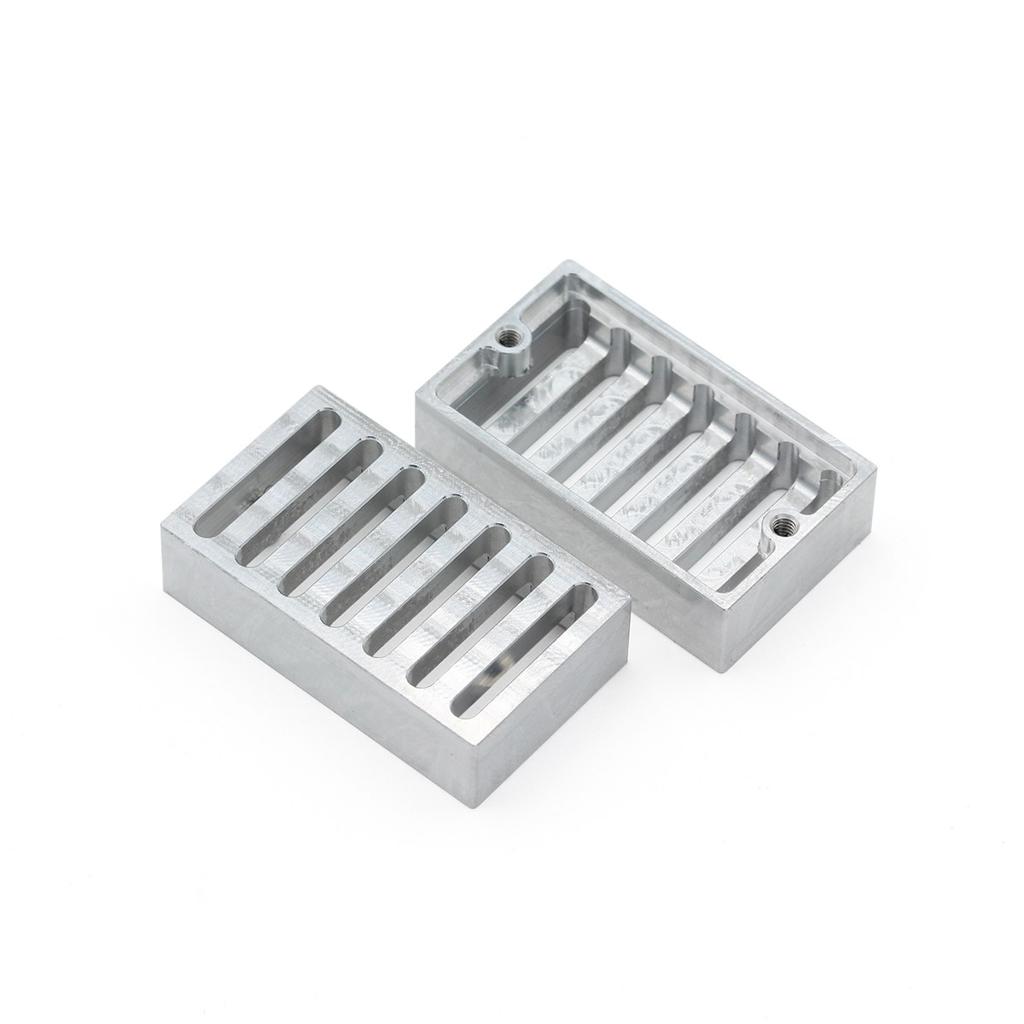
Straight slots, deep grooves, narrow channels, and keyway features with specified widths and depths.
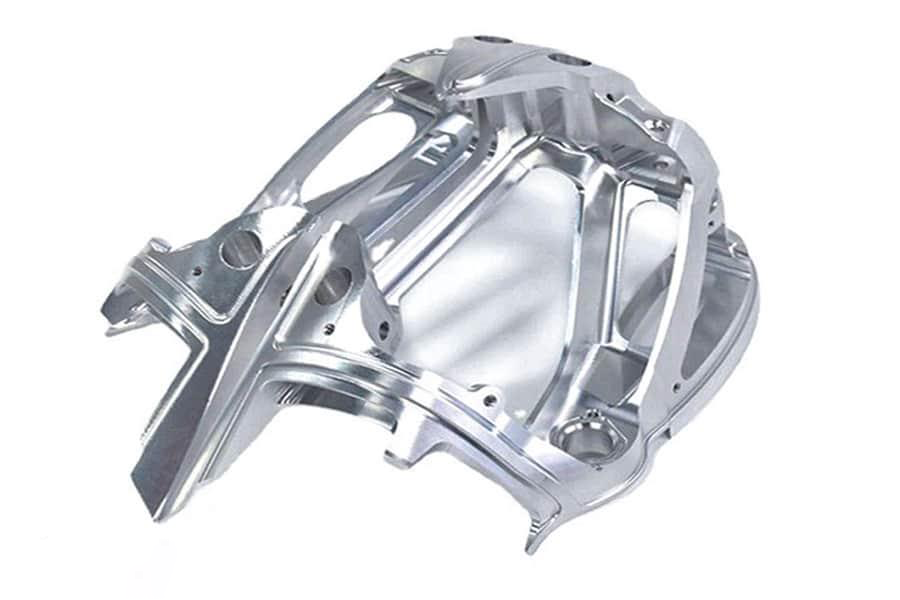
Curved profiles, 3D contours, blended surfaces, and complex geometries requiring multi-axis milling.
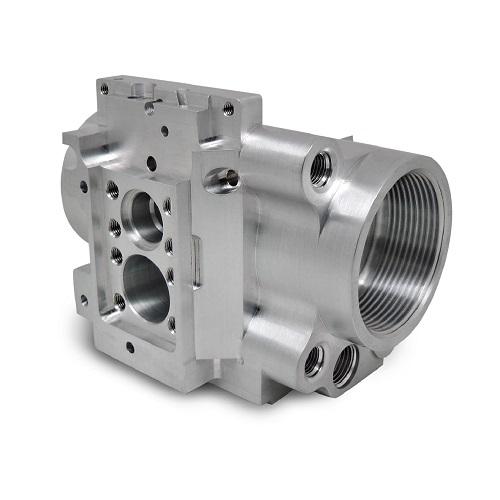
Locating bores, mounting holes, counterbores, countersinks, and internal threads machined to drawing specifications.
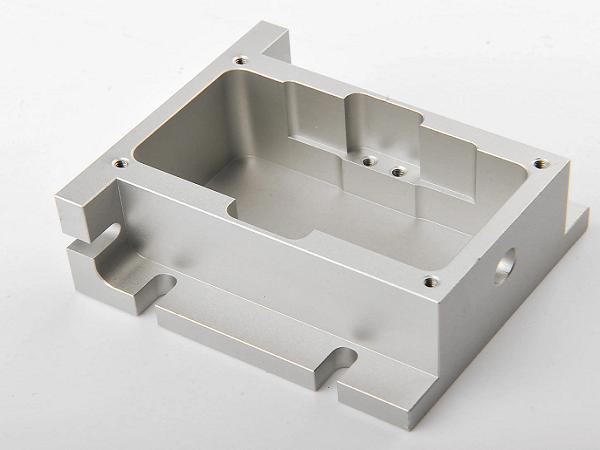
Accessible undercuts, internal reliefs, T-slots, and recessed profiles in custom machined components.
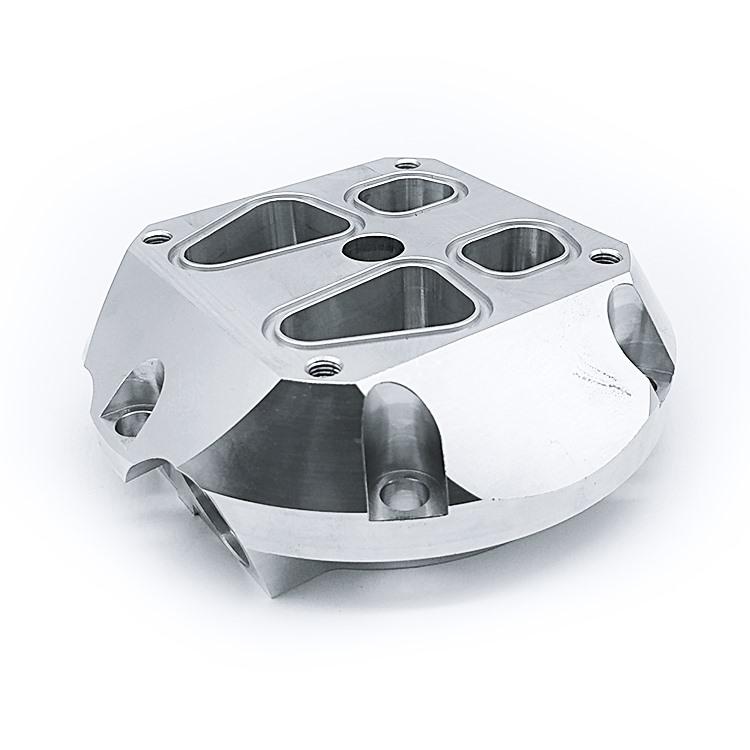
Inclined surfaces, angled holes, and mounting features distributed across multiple faces of a component.
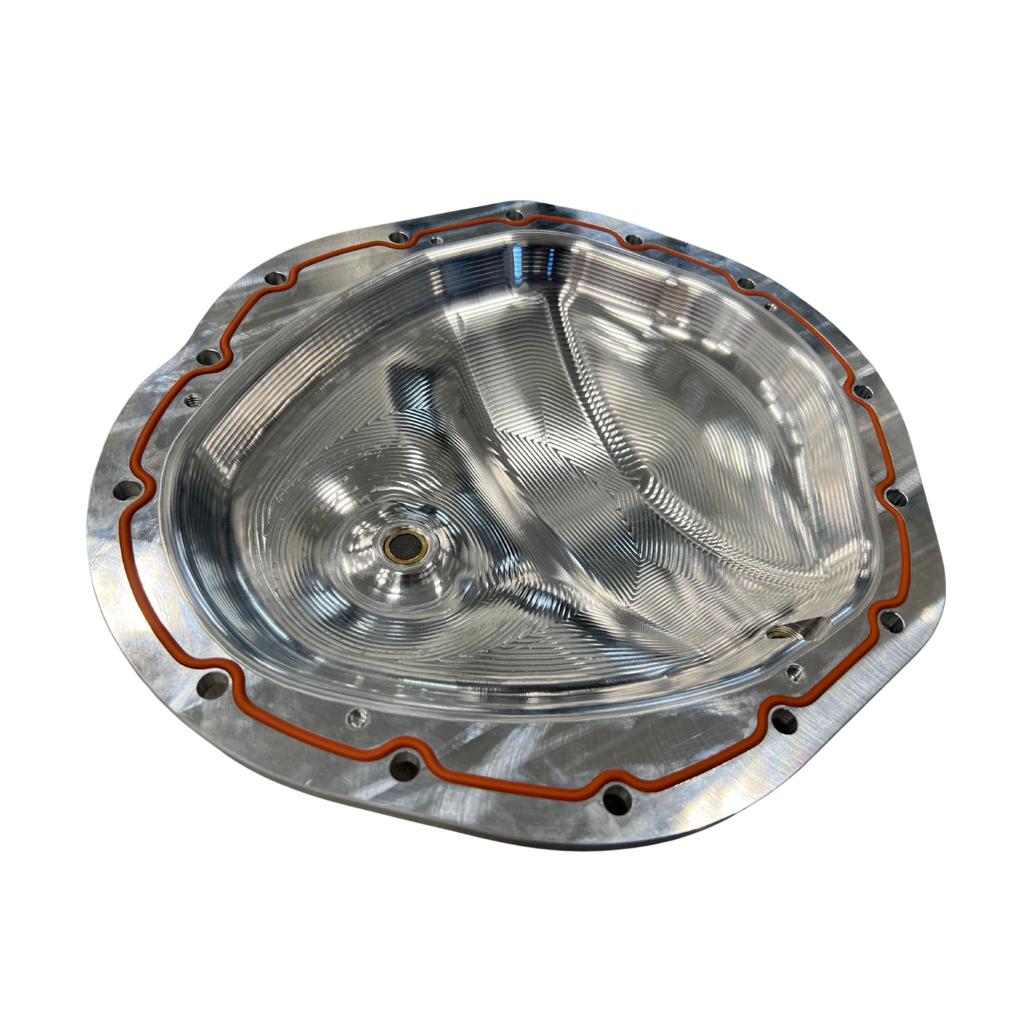
Sealing faces, locating shoulders, mating surfaces, and assembly interfaces with specified dimensional and surface requirements.
MS Machining provides CNC milling for aluminum, stainless steel, carbon and alloy steel, brass, copper, and engineering plastics. Parts can be supplied with standard as-machined surfaces or finer milled finishes according to drawing requirements. Surface finish is determined by material, part geometry, and the specified roughness of individual features.
| Material | Common Grades |
|---|---|
| Aluminum Alloys | 6061-T6, 7075-T6 |
| Stainless Steel | 304, 316, 17-4 PH |
| Carbon & Alloy Steel | 1018, 1045, 4140 |
| Brass | C360 |
| Copper | C110 |
| Engineering Plastics | POM, PEEK, PTFE, PA6 |
General milled surface with visible machining marks.
Finer surface texture produced by finishing passes.
Fine-milled surface with controlled tool marks and surface texture.
*Ra 0.8 μm is evaluated according to material, part geometry, and surface requirements.
Milling marks may remain visible on as-machined surfaces, even with finer Ra values. For mating faces, sealing surfaces, and other functional features, the required surface roughness should be identified on the engineering drawing.
MS Machining manufactures custom CNC milled parts to customer drawings and specified dimensional tolerances. General tolerances can follow ISO 2768-m, while tighter tolerances down to ±0.01 mm are available for selected critical features. Tolerance requirements are reviewed according to material, part geometry, and feature accessibility.
Permissible deviations for linear dimensions under ISO 2768-1, tolerance class m, where individual tolerances are not specified.
| Nominal Dimension | Permissible Deviation |
|---|---|
| 0.5–6 mm | ±0.1 mm |
| Over 6–30 mm | ±0.2 mm |
| Over 30–120 mm | ±0.3 mm |
| Over 120–400 mm | ±0.5 mm |
| Over 400–1000 mm | ±0.8 mm |
Values shown are selected linear dimension tolerances under ISO 2768-1, class m. Individually specified drawing tolerances take precedence.
Tighter tolerances are commonly specified for locating holes, mating surfaces, mounting features, and other dimensions affecting part assembly.
Deep pockets, thin walls, and multi-sided features may require additional consideration of machining access, workholding, and part rigidity.
Critical dimensions and geometric requirements should be clearly identified on the engineering drawing so that their feasibility can be reviewed before machining.
Find answers to common questions about CNC milling quotations, drawing requirements, order quantities, production lead times, and part manufacturability.
Request a Quote →You can submit a 3D CAD model in STEP (.step or .stp) format, preferably accompanied by a 2D engineering drawing in PDF format. The drawing should identify critical tolerances, threaded features, surface roughness requirements, and any other specifications not fully defined in the 3D model.
Please also include the material, required quantity, and expected delivery date.
High-precision CNC milling is used to manufacture parts with tight dimensional and geometric tolerances, particularly where accurate positioning, alignment, or assembly fit is required.
Compared with general CNC milling, high-precision milling places greater emphasis on toolpath planning, workholding, thermal stability, and the control of critical features. Typical applications include precision housings, locating features, mating surfaces, and components with closely toleranced holes or pockets.
At MS Machining, dimensional tolerances down to ±0.01 mm can be supported on selected features, depending on the material, part geometry, and drawing requirements.
Yes. We support prototype machining for fit checks, assembly testing, and design verification before proceeding to production. If you plan to order additional quantities after prototype approval, please indicate the expected production volume when requesting a quote.
This allows the initial machining approach to be considered alongside potential repeat orders.
CNC milling can accommodate individual prototypes, small batches, and recurring production orders. Minimum quantities and pricing are evaluated according to part complexity, material requirements, tooling, and setup time.
You can submit your required quantity for a project-specific quotation.
Lead time depends on the part geometry, material availability, order quantity, and any additional machining requirements. Parts with deep cavities, multiple setups, or complex features may require more machining time than simpler components.
We review the drawing and requested quantity before confirming the production schedule. Please specify your required delivery date when submitting an inquiry.
CNC milling costs are influenced by material selection, machining time, setup requirements, part complexity, tolerances, and order quantity.
Deep pockets, narrow slots, small internal corner radii, and features requiring multiple setups can increase machining time. If your design allows flexibility in non-critical dimensions or internal radii, these details can be reviewed during quotation to identify possible cost reductions.
Yes. We can review customer drawings for machining accessibility, internal corner radii, thin-wall features, tool clearance, and setup requirements.
Where a feature presents a manufacturing concern, we can discuss possible adjustments before machining. Any proposed changes to the drawing or specifications require customer approval.